

Why do PV combiner boxes need dedicated anti-reverse Schottky modules?
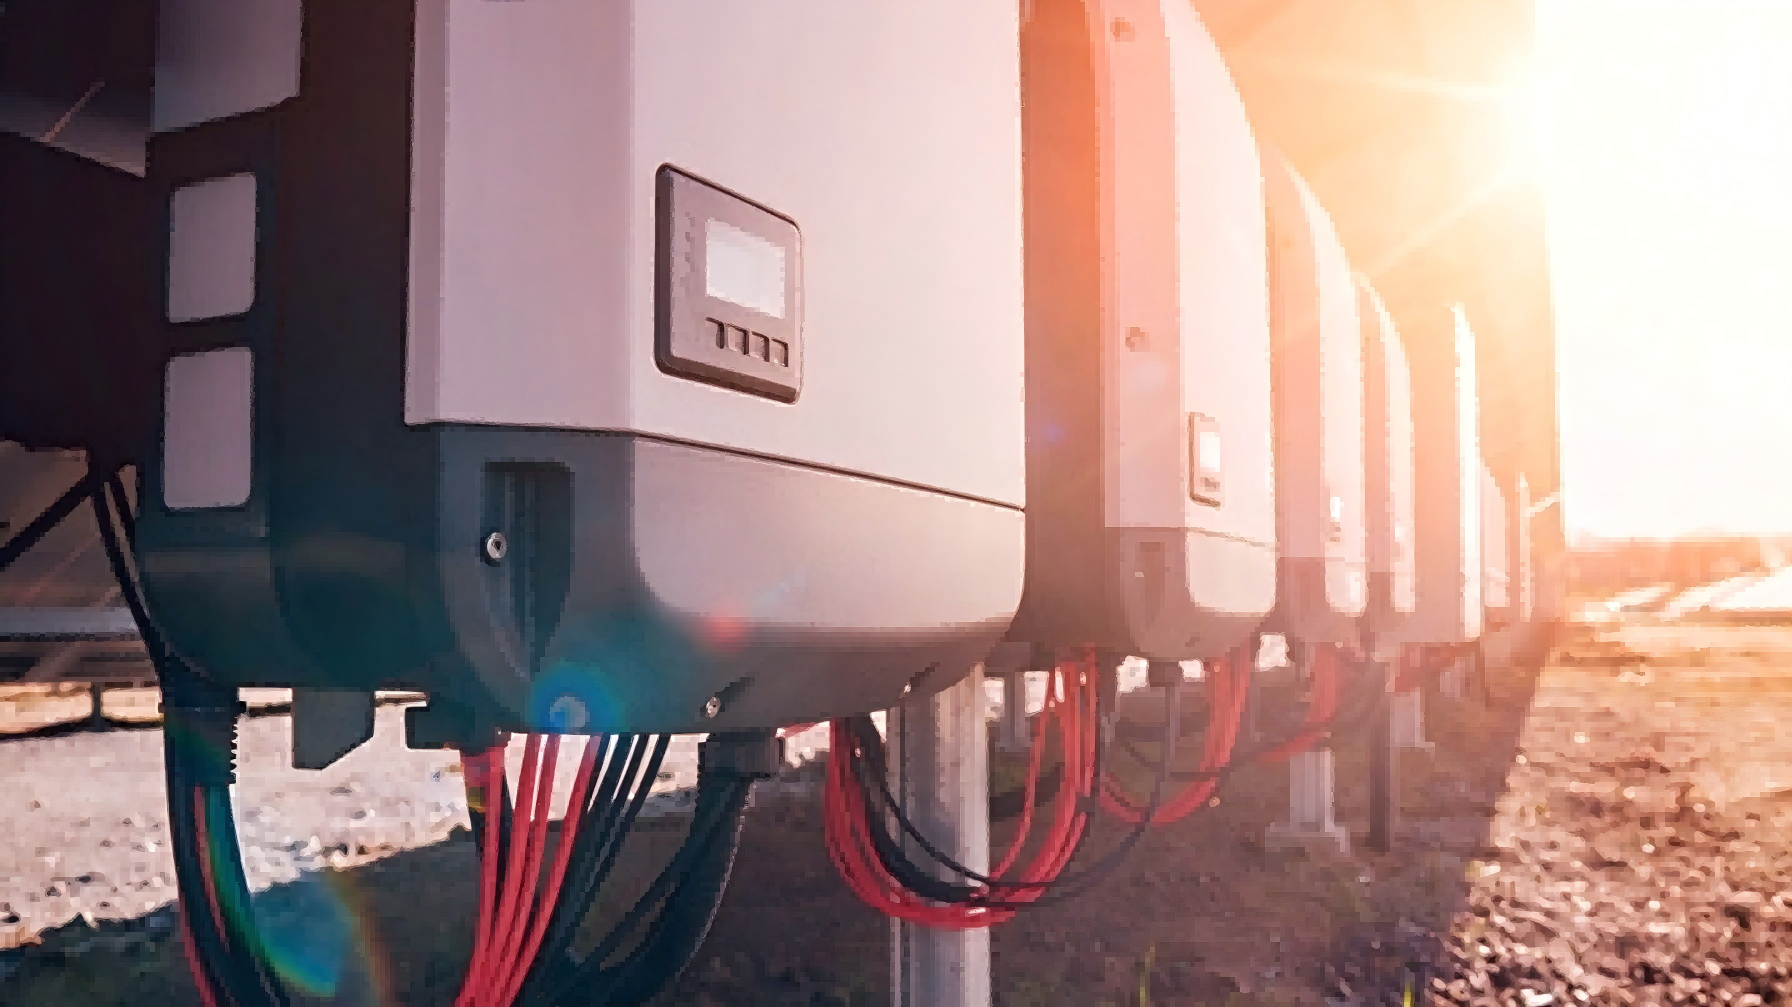
The reverse-blocking diodes inside a combiner box conduct continuously throughout the PV power generation process. To meet outdoor protection requirements, the combiner box uses an IP65 sealed enclosure with virtually no natural convection ventilation. Therefore, the heat generated by the device's forward voltage drop can only be conducted outward through the device's own thermal resistance path. Industry measured data show that for a 16-input/1-output combiner box, assuming 8 A per branch and a forward voltage drop VF of 0.6 V, the total power loss of all reverse-blocking diodes can reach 76.8 W. A large amount of heat accumulating inside the sealed enclosure is one of the important causes of accelerated aging of internal components, temperature drift in sampling circuits, and even enclosure fire in extreme cases.
Discrete-packaged Schottky devices rely on PCB copper foil for heat dissipation; the thermal conduction path is long and the effective heat-dissipation cross-sectional area is limited. When the string operating current reaches 30 A or more, local hot spots are very likely to form at solder joints. Modular Schottky devices integrate multiple chips on an insulated or non-insulated metal baseplate. The thermal conduction path from chip to baseplate is shorter and the heat-conduction cross-section is larger, making them a reliable and feasible heat-dissipation solution for engineering applications in sealed PV combiner boxes.
Selection Criterion #1: Convert VF to the Actual Operating Current
The most fundamental difference between PV-specific reverse-blocking modules and general-purpose diode modules lies in the forward voltage drop parameter. The VF of PV-specific reverse-blocking modules is generally in the 0.76–0.80 V range, while general-purpose diode modules can reach 0.90–0.95 V. For every 0.1 V increase in VF, at a continuous operating current of 30 A, a single branch incurs an additional 3 W of long-term thermal load. The Hypersemi HS8MBRH300N2X100 (M31H package, 300 A/200 V, VFM 0.75 V, IFSM 2000 A, non-isolated SBD) has a relatively low on-state voltage drop among 200 V blocking-voltage-class products and can effectively control the continuous heat source inside the combiner box. If the combiner box uses centralized reverse blocking on a busbar or a multi-branch parallel scheme, devices rated 400 A/200 V with a 3300 A surge rating can be evaluated, using a larger chip area to spread current density and reduce the thermal cycling stress on the device.
Selection Criterion #2: Thermal Resistance and Thermal Cycling Capability Determine "How Long It Lasts"
VF determines how much heat the device generates, while thermal resistance determines whether that heat can be conducted and dissipated effectively. For PV-specific reverse-blocking modules, the maximum thermal resistance from the chip junction to the baseplate can be as low as 0.5 °C/W, while general-purpose diode modules can have thermal resistance as high as 1.3 °C/W. Under the same power loss, the junction-to-case temperature difference between the two can differ by nearly a factor of three. Thermal cycling endurance is also a key indicator that cannot be ignored: PV-specific modules can achieve more than 10,000 thermal cycles, whereas general-purpose diode modules, limited by their internal processes, often achieve only 2,000 cycles or even fewer. PV combiner boxes undergo cyclic temperature rises and falls every day with the day-night ambient environment. Over long-term operation, the difference in thermal cycling capability will manifest as differences in solder-joint fatigue and the probability of device open-circuit failure. Selection should not focus only on the nominal rated current; thermal resistance and thermal cycle count must be treated as hard selection thresholds together with VF.
Selection Criterion #3: Insulation Characteristics Must Match the Mounting Method—Not "the More Insulation, the Better"
If the heat-dissipation baseplate needs to be mounted directly onto the metal enclosure of the combiner box to shorten the heat-dissipation path, using Isolation SBD devices can eliminate the need for additional insulating pads and make assembly easier in narrow enclosures with tight safety clearances. The Hypersemi HS13MBS200N2X100 (M58 package, 200 A/200 V, VFM 1 V, IFSM 1650 A, Isolation SBD) has an integrated insulation structure between the chip and the baseplate, making it suitable for design approaches where the baseplate directly contacts the enclosure for heat dissipation. Non-isolation SBDs, such as the HS8MBRH300N2X100 mentioned above, are suitable for operating conditions where the system is already equipped with an independent insulation structure, and offer lower thermal resistance and cost advantages. The correct selection approach is: first determine the overall system heat-dissipation path, then select the device insulation type, and finally finalize parameter confirmation based on forward voltage drop and surge current. Complete product specifications can be filtered on the Hypersemi official website Schottky module page by combinations of blocking voltage, on-state current, surge current, and insulation characteristics to find matching models.