HG40T120TPX100 in Inverter Welders: Arc Strike, Thermal Management, and Lightweighting
Addressing three real pain points in 160-250A inverter welders - slow arc strike, thermal runaway at elevated temperature, and heatsink volume - the HG40T120TPX100 delivers a discr
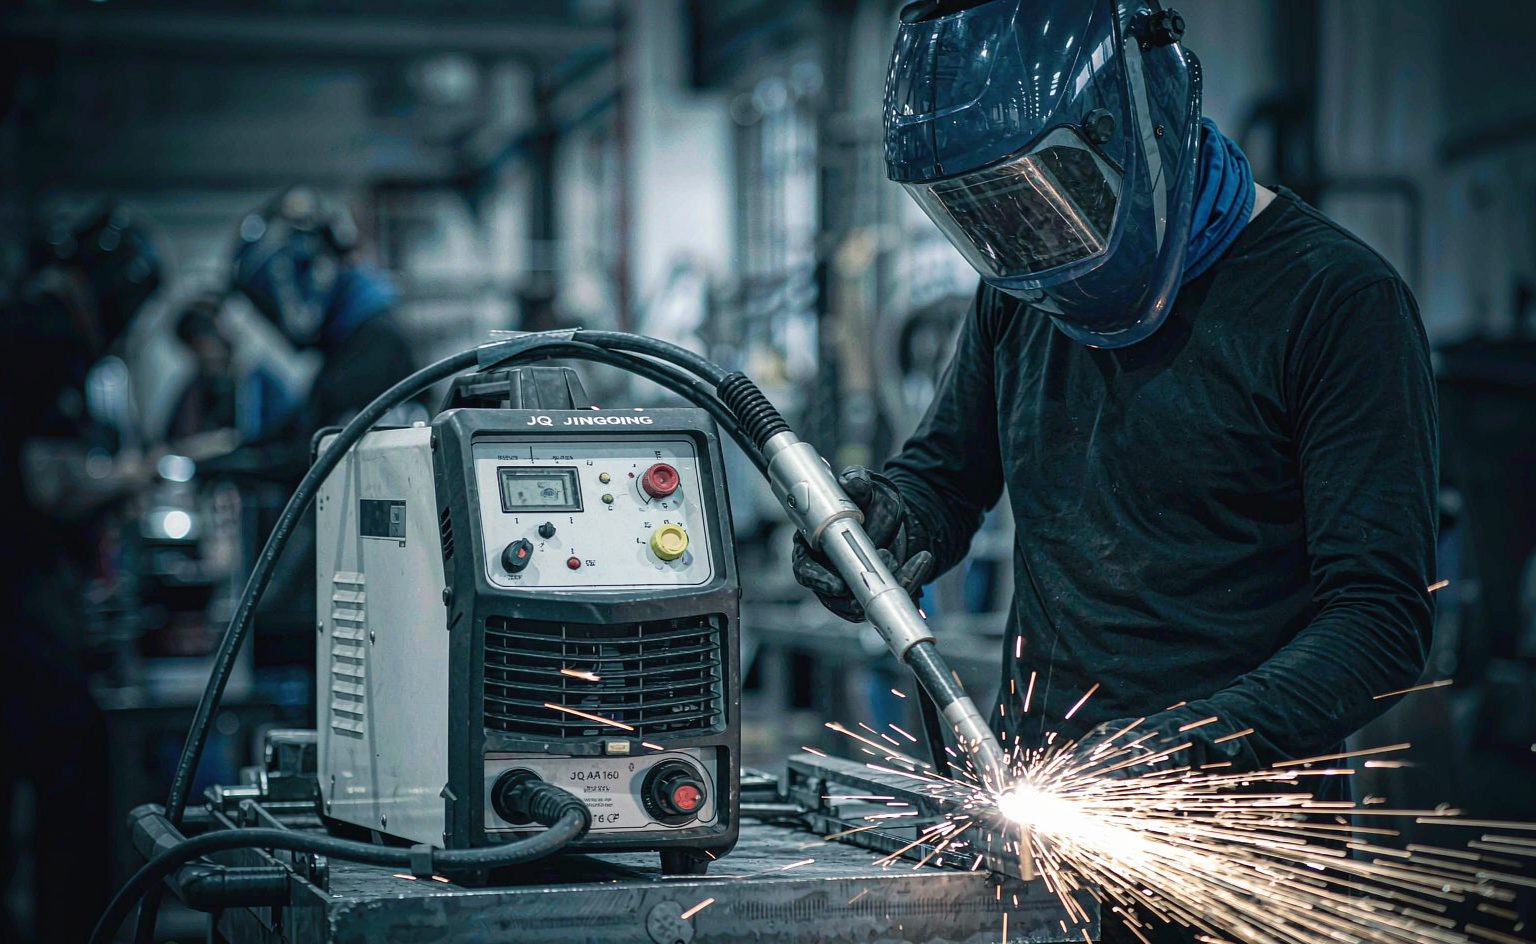
Addressing three real pain points in 160-250A inverter welders - slow arc strike, thermal runaway at elevated temperature, and heatsink volume - the HG40T120TPX100 delivers a discrete solution with 21ns-class turn-on, 175C junction capability, and 0.28K/W thermal resistance.
Bottom Line First: When Is an IGBT Discrete the Right Choice for a Welder?
If your welding machine meets the conditions below, a 1200V / 40A IGBT discrete such as the HG40T120TPX100 is the mainstream choice today:
- Output range of 160–250A — discrete solutions hold a clear cost advantage in small and mid-power inverter welders
- Portability matters — discretes are lighter than modules and offer free layout, making a sub-5kg machine far easier to achieve
- Duty cycle of 60% or higher — thermal design is manageable for discretes in this range
Conversely, for a 400A-and-above heavy-duty industrial welder, or where 100% duty cycle continuous welding is required, go directly to a 34mm or 62mm module solution. Discretes do not have sufficient thermal headroom in that regime.
Three Real Engineering Pain Points in Inverter Welders
When welder manufacturers iterate on a design, they never face a single problem — they face three stacked together:
- Arc-strike success rate is limited by device switching speed. Long switching delay means current builds slowly at ignition, producing lack of fusion at the start of the weld bead.
- Thermal runaway at elevated temperature. Welding is a pulsed high-current duty. Devices heat up repeatedly across an 8-hour shift, and parameter drift accumulates with every cycle.
- The cooling system consumes chassis space. The heatsink often occupies more than 40% of total machine volume, directly conflicting with portability targets.
The HG40T120TPX100 was designed against exactly these three constraints.
Five Key Characteristics of the HG40T120TPX100
1. Saturation Voltage: 2.5V @150℃
Trench-gate field-stop technology paired with an optimized FRD. At 40A continuous, saturation voltage stays at 2.5V @150℃ — roughly 17% lower than conventional solutions.
More importantly, the device has a positive temperature coefficient: voltage drop rises with temperature, so paralleled devices share current automatically and there is no runaway "hotter means more conductive" cycle.
2. Switching Speed: 21ns Turn-On Delay
Turn-on delay plus rise time totals roughly 21ns + 48ns, an improvement of about 69% over conventional solutions. Current builds faster at arc ignition, which raises the arc-strike success rate.
An integrated 2.5Ω gate resistor suppresses drive oscillation, and a ±20V wide gate voltage range keeps it compatible with mainstream driver ICs, lowering the barrier for peripheral circuitry.
3. High-Temperature Reliability: 175℃ Junction Capability
Maximum junction temperature of 175℃, 40% above the conventional 125℃ device. This permits full-load operation at 60℃ ambient, with MTBF for thermal failure well above the industry average.
4. Switching Losses: Eon + Eoff ≤ 5.1mJ
Total switching loss stays under 5.1mJ at 150℃. Together with the integrated fast-recovery diode (VF = 1.8V @150℃), freewheeling-loop loss drops by roughly 22%.
5. Package and Thermal Resistance
TO-3PN package (15.9 × 5.44mm) with thermal resistance of 0.28K/W (IGBT) and 0.55K/W (diode). Mounting area is roughly 60% smaller than legacy large packages, leaving room for paralleling. Pulsed current capability of 160A handles the surge at weld initiation.
Key Parameters at a Glance
| Parameter | Value | Test Condition |
|---|---|---|
| Blocking voltage VCES | 1200V | — |
| Continuous current IC | 40A | TC=100℃ |
| Pulsed current ICM | 160A | — |
| Saturation voltage VCE(sat) | 2.5V | 40A / 150℃ |
| Turn-on delay td(on) + rise tr | ≈ 69ns | 150℃ |
| Total switching loss Eon+Eoff | ≤ 5.1mJ | 150℃ |
| Maximum junction temperature Tj,max | 175℃ | Continuous |
| Thermal resistance Rth(j-c) | 0.28K/W | IGBT |
| Thermal resistance Rth(j-c) | 0.55K/W | Diode |
| Package dimensions | 15.9 × 5.44mm | TO-3PN |
Application Case: 250A Portable Inverter Welder
Design targets: stable arc ignition at 3000m altitude, 100% duty cycle, total machine weight under 5kg.
Measured results:
- Full-load efficiency 93.5% (tested to EN 50598)
- Critical-component temperature rise ≤ 72K after 8 hours of continuous welding at 40℃ ambient
- Arc-strike success rate with 3.2mm electrodes: 100% under ±15% line voltage fluctuation
- Total machine weight 4.7kg, heatsink volume reduced 52% versus the previous generation
What underpins this result is the positive temperature coefficient of VCE(sat) — only 2.5V at 150℃ means the welder does not suffer progressively worsening efficiency during prolonged high-temperature work. For continuous-duty environments such as mining and shipbuilding, that is decisive.
Two Points Most Often Overlooked During Selection
1. Duty Cycle, Not Rated Current, Drives Device Selection
Welders are classic intermittent-load equipment. In two 250A machines, a 60% duty cycle and a 100% duty cycle impose thermal demands that differ by more than a factor of two. Select against the worst-case continuous welding condition rather than the nameplate rating. If thermal headroom is insufficient, the machine trips its over-temperature protection mid-job — which users experience simply as "it stops while I'm welding".
2. Tune the Gate Resistor and Arc-Ignition Timing Together
The integrated 2.5Ω gate resistor is a default. The current build-up rate at arc ignition is determined jointly by gate resistance, drive voltage, and bus voltage. Configuring peripherals purely from the datasheet rarely gives optimal arc performance. We recommend observing VCE and IC waveforms at ignition with an oscilloscope during prototyping, then back-calculating the optimal gate resistance.
Frequently Asked Questions
Can a discrete solution reach 300A output?
Yes, with paralleling. The current capability of a discrete solution depends on the number of paralleled devices and the thermal design. Paralleling works well with positive-temperature-coefficient devices because current self-balances. However, more devices in parallel raise drive-circuit complexity and routing difficulty, so from a combined cost-and-reliability standpoint, module solutions are usually more economical above 300A.
Why emphasize "trench field-stop" rather than trench gate alone?
The field-stop layer thins the drift region while maintaining high blocking voltage, lowering conduction drop and switching loss simultaneously. A pure trench-gate structure at the 1200V class typically forces a trade-off between drop and switching speed. Only the combination delivers both low loss and fast switching at high blocking voltage — which is the foundation for high-frequency welder topologies.
How should the 175℃ junction rating be used in practice?
Do not treat 175℃ as a normal operating point. Its real value is transient headroom: at arc ignition or load steps, junction temperature spikes briefly, and 175℃ tolerance keeps those transients from causing failure. Steady-state thermal design should still keep junction temperature under 125℃, preserving a 50℃ transient buffer.
Summary
The HG40T120TPX100 is positioned as a discrete solution for 160–250A inverter welders that balances efficiency, portability, and high-temperature reliability. Its value is not leadership in any single parameter but the combination of a positive-temperature-coefficient saturation voltage, 21ns-class switching speed, and 175℃ junction capability — letting a welder be both small and continuously productive.
Need a thermal design calculation for a specific machine? Tell us your output current, duty cycle, and chassis dimensions, and we will recommend a matching device combination.